
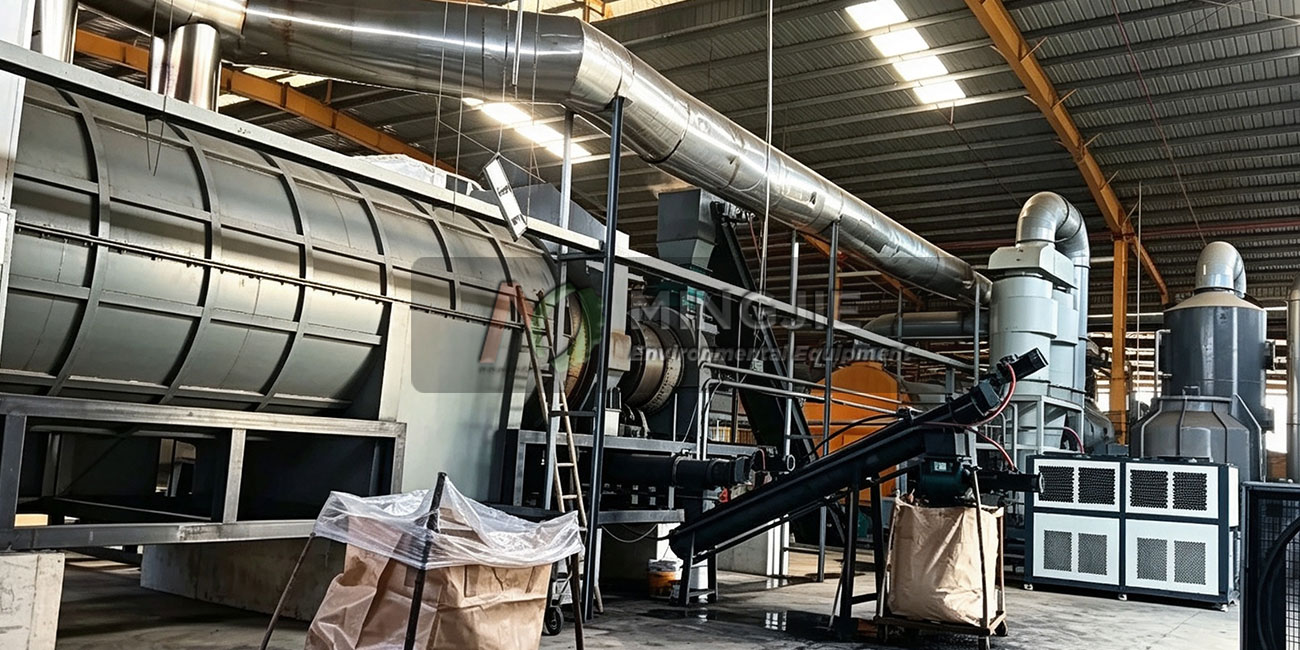
Technical Specifications
| Model | MJT-100 | MJT-500 | MJT-1000 | MJT-2000 | MJT-3000 | MJT-5000 |
| Capacity | 100KG/H | 500KG/H | 1000KG/H | 2000KG/H | 3000KG/H | 5000KG/H |
| Operation | Fully Continuous | |||||
| Accepted materials | Rice Husk, Saw Dust, Wood Waste, Straw, Palm Shell, Coconut Shell, Sludge, Animal Manure, Sugarcane Bagasse | |||||
| End products | Biochar, Syngas, Tar& Wood Vinegar(optional) | |||||
| Applicable fuel | Coal/Natural Gas/LPG/Diesel/Wood/Pyrolysis Oil | |||||
| Material of reactor | 304 Stainless Steel | |||||
| Reactor structure | Double Cylinders | |||||
| Cooling | Water Cooling | |||||
| Land Required | 300-400m2 | |||||
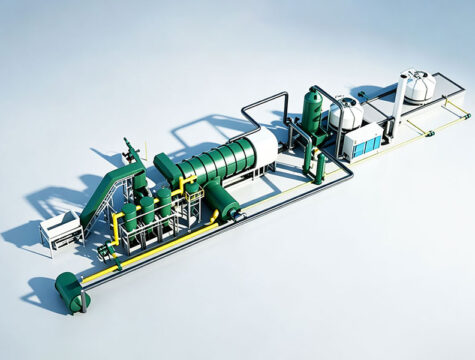
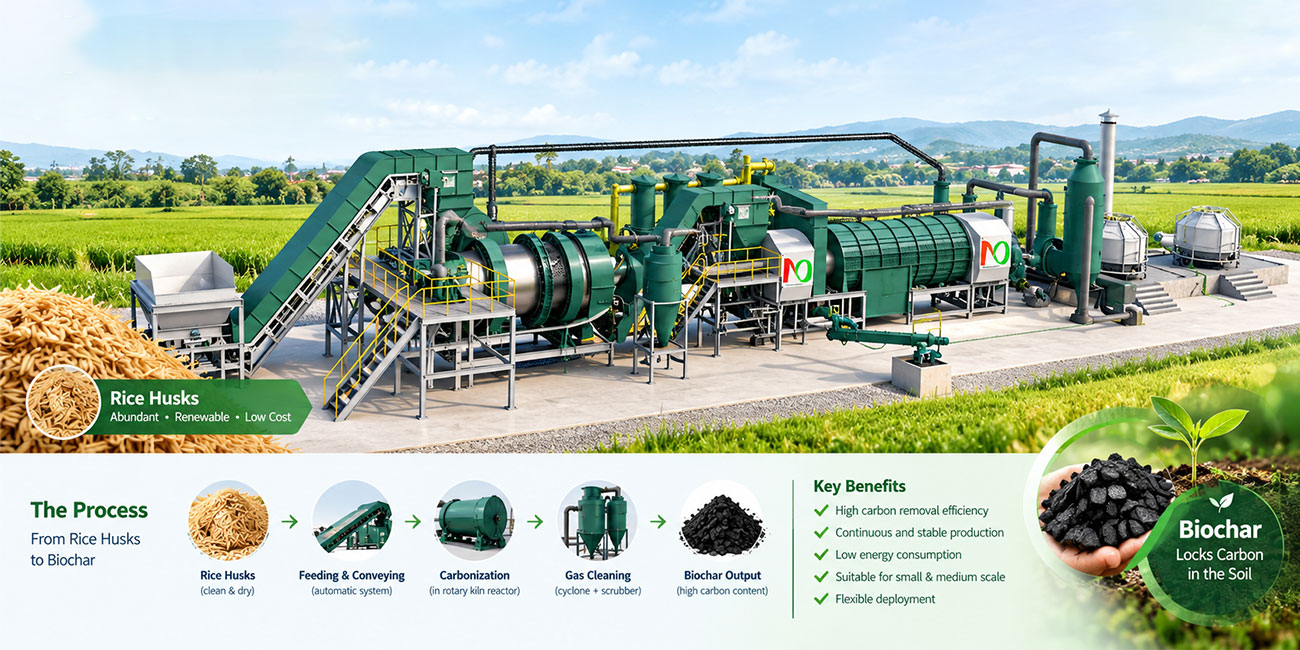
Rice husk biochar production plant, integrated with dMRV monitoring systems, transforms rice husks from waste into tradable, verifiable, and long-lasting carbon removal assets. The rice husk biochar production equipment utilizes a continuous pyrolysis process to achieve large-scale biochar production. Rice husk feedstock enters at one end, passes sequentially through drying, preheating, carbonization, and cooling zones within the furnace, and is continuously discharged from the other end.
Raw Materials
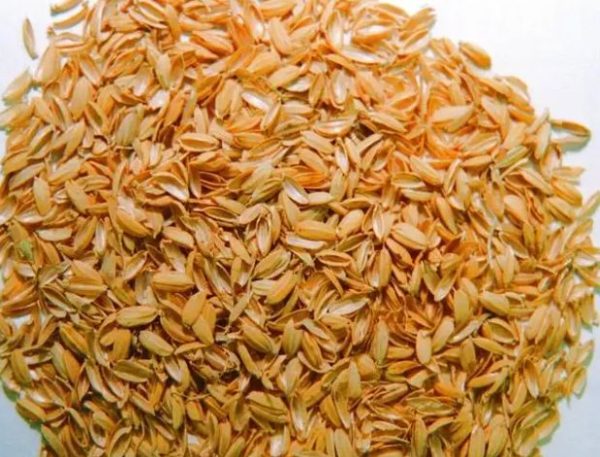
Rice husks are among the most suitable agricultural and forestry waste feedstocks globally for biochar-based carbon removal projects. As a by-product of rice processing, they feature concentrated sourcing, stable production volumes, and consistent properties.
What distinguishes rice husks most significantly from other agricultural wastes is their exceptionally high silicon content. Following pyrolysis, silicon dioxide remains within the rice husk biochar in an amorphous state, often constituting over 35% of the material.
Silicon significantly enhances the disease resistance of rice plants. Furthermore, silicon dioxide acts as a natural template, facilitating the formation of a hierarchical pore structure within the biochar.
Final Products
|
Name |
Picture |
Application |
|
Rice Hull Biochar |
|
Used as soil conditioner, carbon sequestration, improve the quality of soil Used as fuel for industry heating and cooling or BBQ Can be reprocessed into activated carbon, widely used in the smelting, chemical fields. |
|
Tar & Wood vinegar |
|
Widely used as a crop insecticide, make leaf surface fertilizer |
|
Syngas |
|
Can be recycled to heat the carbonization host. By this way, you can reduce a lot of fuel costs. |
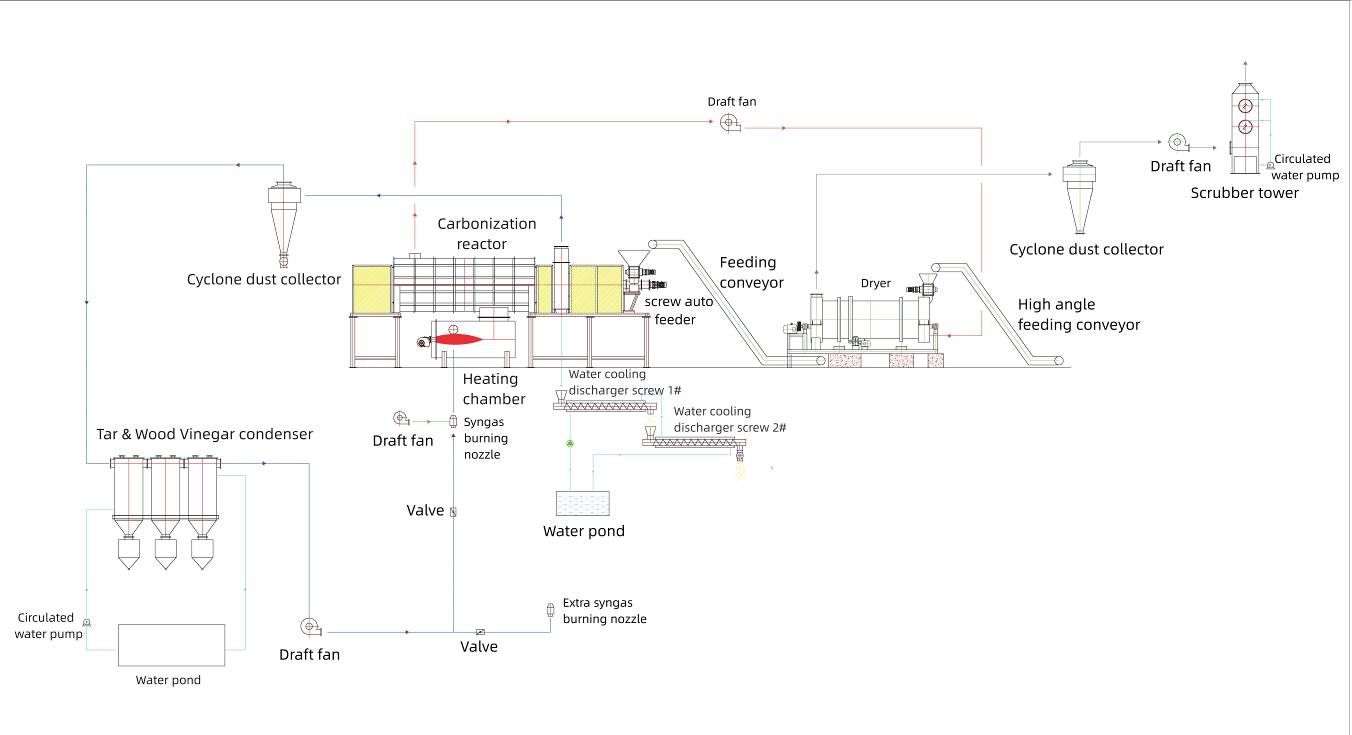
Flowing Diagram
Core Modules for Large Scale Rice Husk Biochar Production Plant
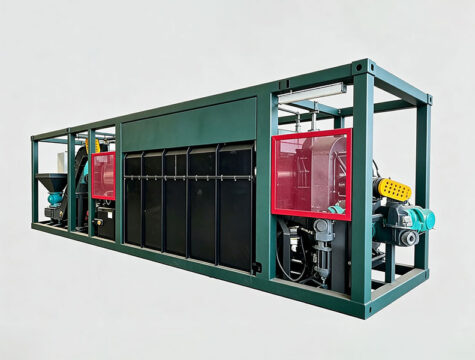
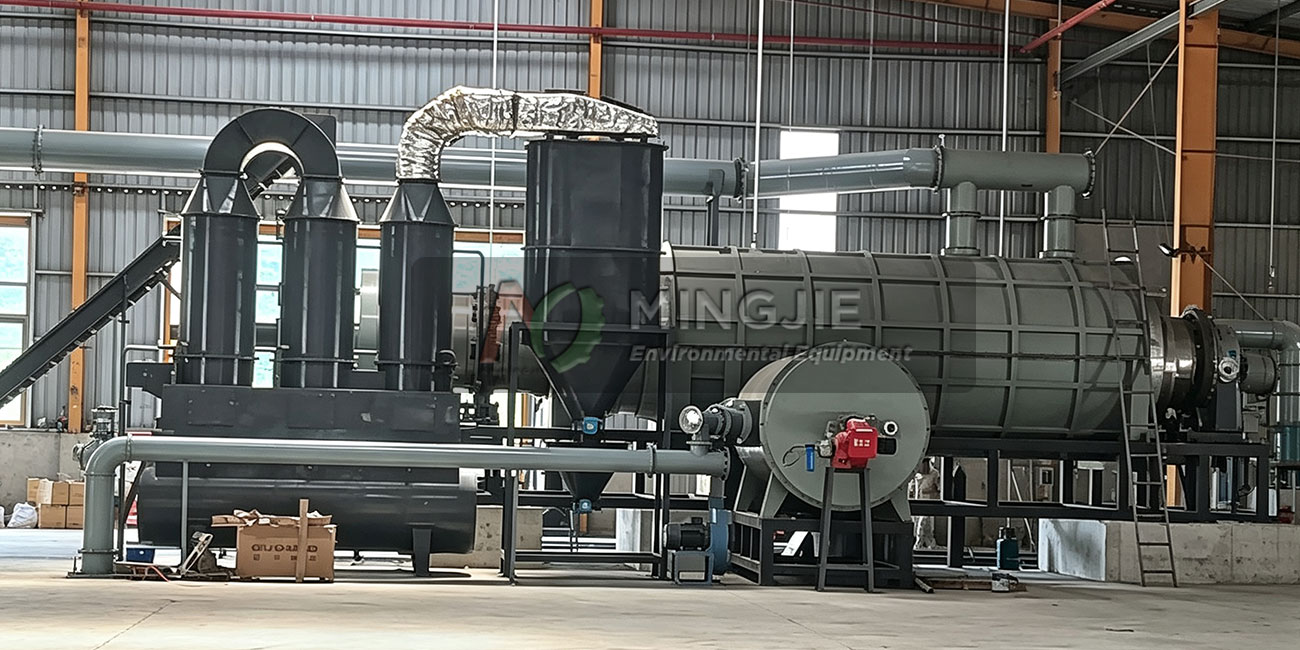
The large scale biochar production plant comprises a feeding system, a carbonization reactor, a syngas purification and recovery system, a cooling and discharge unit, an exhaust gas treatment system, and a PLC control cabinet.
Pre-treatment Unit: Regulates the moisture content of rice husks within a stable range to prevent raw material agglomeration and incomplete combustion.
Feeding System: Utilizes a sealed airlock structure to prevent dust emissions and the ingress of air into the reactor.
Pyrolysis Reactor: Employs a continuous slow pyrolysis process with the temperature strictly controlled between 500°C and 600°C. Precise control of residence time ensures the desired degree of biochar aromatization, meeting the H/Corg ratio requirements for carbon removal projects.
Syngas Recovery and Utilization System: Syngas generated during pyrolysis is purified and recirculated for combustion to provide process heat. This enables energy self-sufficiency, with surplus heat available for the drying stage.
Biochar Cooling and Discharge System: As the carbonized rice husks exit the reactor at high temperatures, the resulting biochar must be cooled prior to discharge.
Tail Gas Treatment Unit: Tail gas undergoes dust removal and purification to ensure emissions meet regulatory standards, preventing pollutant discharge from negatively impacting the project's ESG assessment.
dMRV System
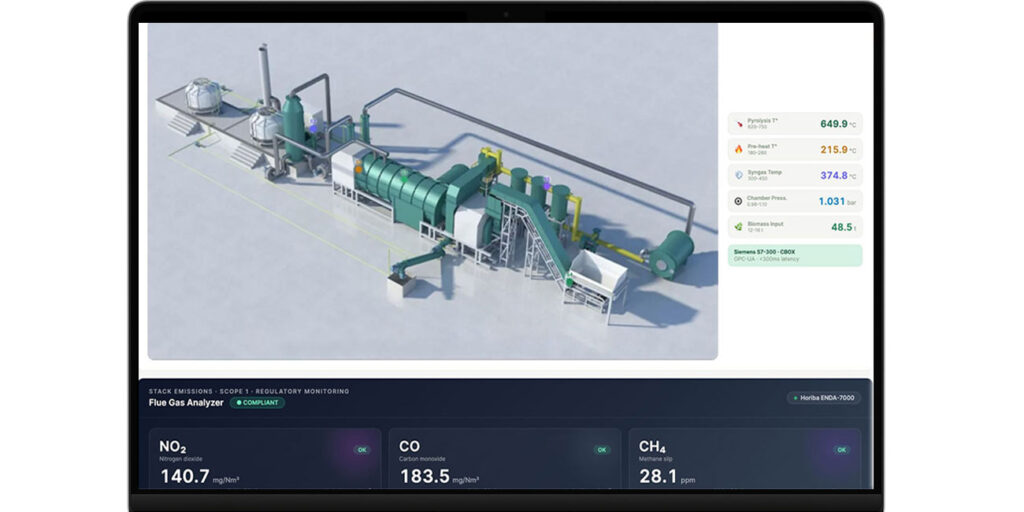
Customized Solutions for Top clients:
- Comprehensive data collection, visualization, and management.
- Premium equipment, PLCs, expanded sensor arrays, Cbox hardware, and after-sales service.
The rice husk biochar production plant utilizes an integrated dMRV system to centrally manage data regarding operations, production, emissions, and carbon removal. Mingjie offers a highly cost-effective package: equipment paired with dMRV configuration, high-integrity carbon credits, rapid deployment and scalability, and "bankable" dashboards that meet investor standards.
The dMRV system addresses the challenges of trust and management associated with scaling up biochar carbon removal (BCR) projects, enabling full lifecycle traceability of the biomass. The quality of carbon credits generated by biochar projects depends heavily on the sustainability of feedstock sources, compliance during production, and whether the end-use effectively sequesters carbon.
The dMRV system enables digital tracking across the entire biochar value chain, covering every stage from biomass sourcing, production, and transportation to final application. This end-to-end traceability provides the foundational data to substantiate the authenticity of the carbon credits.
Our Advantages
Advantages of Biomass Pyrolysis Carbonization Plant
Reactor structure takes dual cylinder type, which has long stroke and can ensure the biomass carbonized completely
Complete Reactor made of 304 stainless steel, which can resist high temperature and give the machine service life much longer
Fully Continuous operation, non-stop running, keep feeding and carbon discharging 24 hours per day, high automation,
The complete line takes modular design, which is easy for transportation and installation, save a lot of installation cost
The machine use it own produced syngas as main fuel during the carbonization, save a lot of energy cost
PLC control system, the process is fully automatic